


THE ROLE OF CHILLERS IN THE BEVERAGE MANUFACTURING INDUSTRY
During beverage production, temperature directly affects raw material quality, flavor, color, and the consistency of the final product. Many production stages require precise temperature control to ensure that chemical reactions, biological processes, and ingredient dissolution occur under optimal conditions.
Chiller systems provide a stable supply of chilled water to heat exchangers, mixing tanks, filling lines, and various auxiliary systems. This enables the entire production line to operate continuously at high efficiency while maintaining consistent product quality across every production batch.
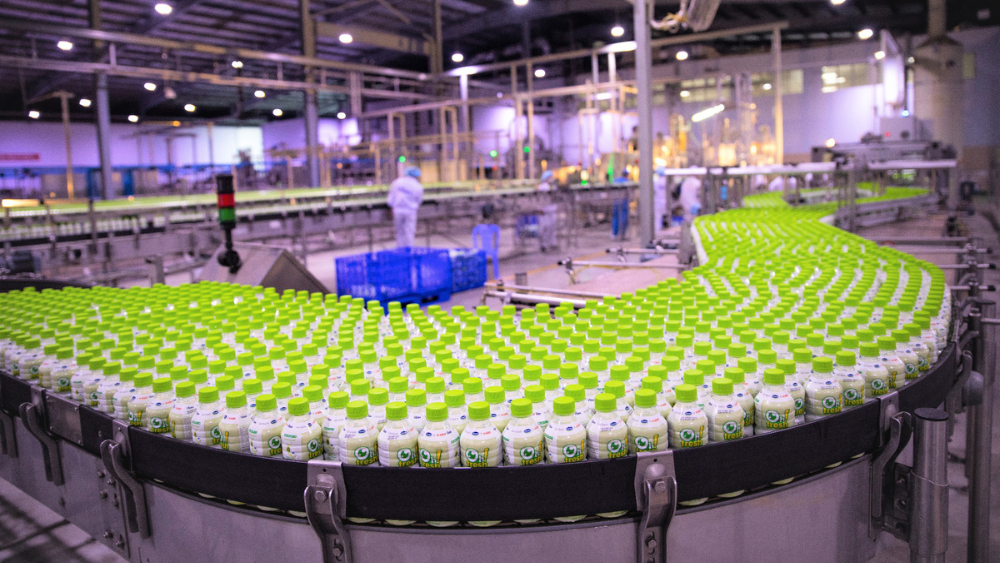
TEMPERATURE CONTROL DURING MIXING AND PROCESSING
During ingredient mixing, many beverages must be maintained within a specific temperature range to ensure the proper dissolution of sugar, flavorings, colorants, and nutritional ingredients.
If the temperature becomes too high or fluctuates significantly, ingredient properties may change, affecting both product quality and taste. Chillers provide precise temperature control throughout the processing stage, ensuring that products meet quality standards before moving to the next production step.
CHILLER APPLICATIONS IN THE FERMENTATION PROCESS
For breweries, fermented beverage manufacturers, kombucha producers, and other specialty beverage facilities, temperature control during fermentation is essential for product quality.
Microorganisms thrive only within specific temperature ranges. If temperatures exceed acceptable limits, the fermentation process may become unstable, resulting in inconsistent flavor, lower product quality, and reduced production efficiency.
Chiller systems maintain optimal temperatures inside fermentation tanks, ensuring a stable fermentation process and consistent product quality.
RAPID COOLING AFTER PASTEURIZATION
Following the pasteurization process, many beverages must be cooled rapidly to preserve product quality, inhibit microbial growth, and prepare the products for packaging.
Chillers provide chilled water for heat exchangers and rapid cooling systems, allowing beverages to quickly reach the required temperature while preserving their flavor and nutritional value.
This process plays an important role in extending product shelf life and ensuring high-quality products reach consumers.
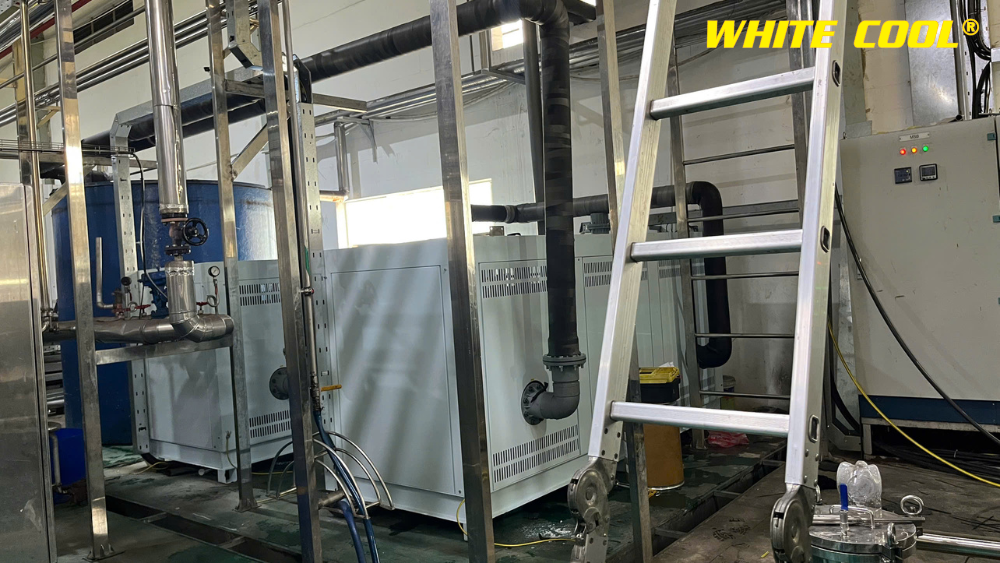
COOLING PRODUCTION EQUIPMENT AND MANUFACTURING LINES
In addition to cooling beverages, Chillers are widely used to cool production equipment such as filling machines, capping machines, PET bottle blowing machines, air compressors, hydraulic systems, and automated production lines.
Maintaining stable operating temperatures allows equipment to perform at maximum efficiency, reduces the risk of overheating, minimizes mechanical wear, and extends equipment lifespan.
This is particularly important for beverage factories operating multiple production shifts each day.
CHILLERS HELP REDUCE ENERGY CONSUMPTION AND OPERATING COSTS
Electricity represents one of the largest operating expenses in beverage manufacturing facilities.
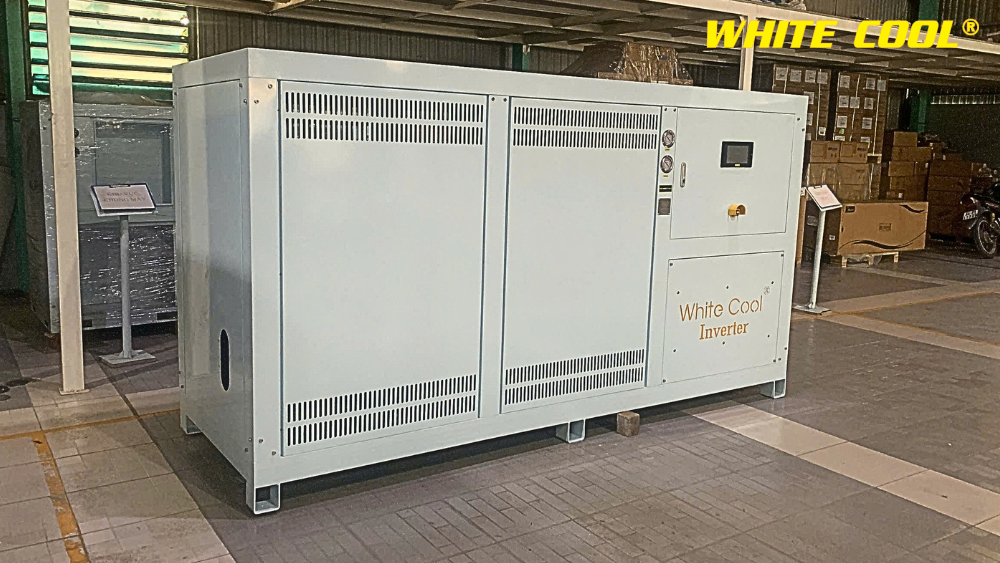
Modern Chiller systems are equipped with Inverter technology, intelligent PLC controls, and the ability to automatically adjust cooling capacity based on actual cooling demand. As a result, the system consumes only the energy required at any given time while maintaining excellent cooling performance.
In addition, a properly designed Chiller system helps reduce maintenance costs, extend equipment lifespan, and lower the Total Cost of Ownership (TCO).
THE TREND OF SMART CHILLERS IN BEVERAGE MANUFACTURING
Automation and digital transformation are becoming increasingly important in the food and beverage industry.
Many modern Chiller systems are integrated with PLC, HMI, SCADA, and IoT technologies to monitor temperature, pressure, water flow, energy consumption, and operating conditions in real time.
By collecting and analyzing operational data, manufacturers can implement predictive maintenance, identify abnormalities early, and optimize the overall performance of their cooling systems.
These intelligent solutions help beverage plants increase productivity, reduce downtime, and meet the demands of modern manufacturing.
WHITE COOL – OPTIMIZED CHILLER SOLUTIONS FOR THE BEVERAGE MANUFACTURING INDUSTRY
Our experienced engineering team conducts cooling load assessments, analyzes production processes, and designs customized Chiller systems for each production line to ensure stable cooling performance, energy efficiency, and long-term reliability. Every Chiller system undergoes comprehensive testing, commissioning, and performance verification before delivery to ensure maximum efficiency and dependable operation.
In addition to Chiller design and manufacturing, White Cool provides installation, preventive maintenance, PLC control system upgrades, and comprehensive after-sales technical support. We are committed to delivering advanced cooling solutions that improve product quality while minimizing operating costs.
If your company is planning a new beverage production facility or upgrading an existing cooling system, contact White Cool to receive professional consultation and a customized Chiller solution tailored to your production requirements.
CONCLUSION
In the beverage manufacturing industry, Chillers play a critical role in controlling the temperature of raw materials, production equipment, and the entire manufacturing process. From mixing and fermentation to pasteurization, rapid cooling, and equipment cooling, Chiller systems help ensure consistent product quality, improve productivity, and maintain stable production operations.
Investing in a properly designed Chiller system enables manufacturers to reduce energy consumption, lower operating costs, extend equipment lifespan, and maximize long-term return on investment. With extensive experience in designing, manufacturing, and implementing industrial Chiller systems, White Cool is ready to support businesses with modern, reliable, and energy-efficient cooling solutions that meet the increasingly demanding standards of the beverage manufacturing industry.